
End-to-end solutions for
global health leaders.
From private labelling and turnkey batch scaling to international regulatory dossiers and high-barrier smart packaging.
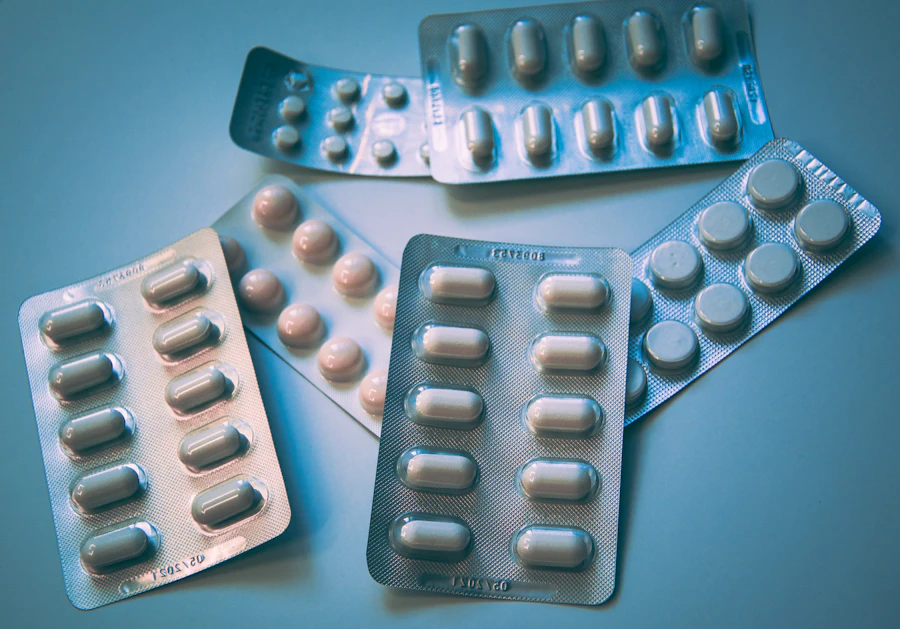
Private Labelling & Brand Scaling
Turnkey formulation, bespoke flavoring & shelf-ready delivery
We are a leading full-service private label manufacturer. Whether you are an early-stage direct-to-consumer brand or an established multinational health enterprise, we deliver custom dosage forms, compliant labeling, and shelf-ready packaging with fast turnaround.
Core Capabilities & Deliverables:

Global Regulatory Dossiers & Filings
FSSAI, AYUSH, US FDA 21 CFR 111 & EFSA dossier preparation
Ensure seamless market entry with our in-house regulatory affairs specialists. We work directly with international health authorities to provide comprehensive documentation, stability validation, and nutritional claims compliance.
Core Capabilities & Deliverables:
CRAMS (Contract Research & Cleanroom Scaling)
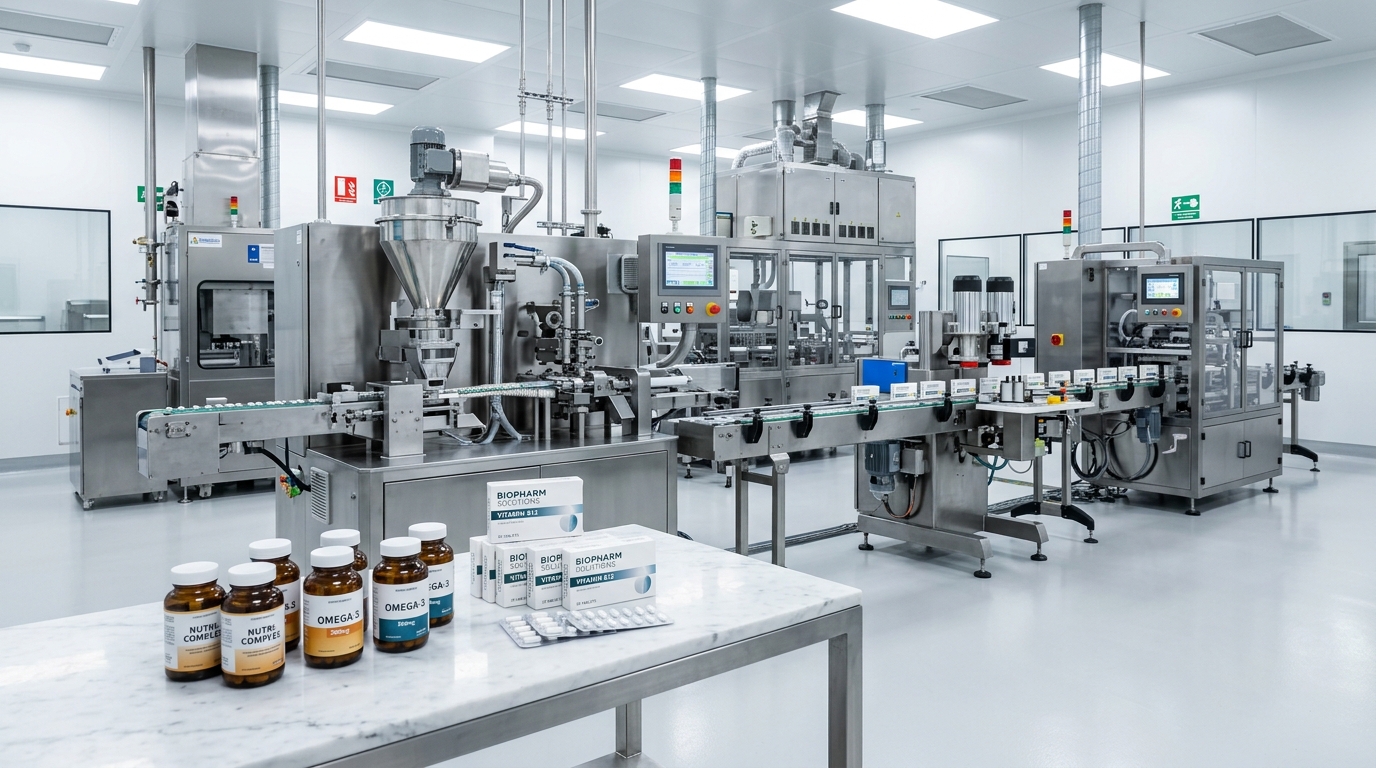
Class 100,000 cleanrooms, UHPLC assay testing & commercial batching
A trusted contract research and manufacturing partner with high-precision cleanroom facilities. From benchtop molecule synthesis to multi-ton commercial production in WHO-GMP cleanrooms, we scale your proprietary formulations with zero compromise.
Core Capabilities & Deliverables:
High-Barrier Packaging & Smart Delivery
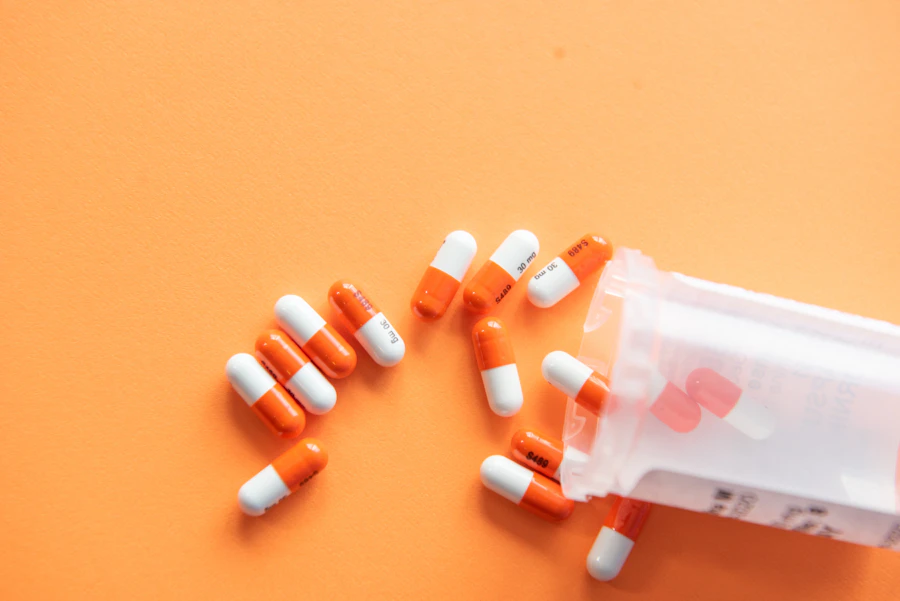
Alu-Alu blisters, nitrogen-flushed stick packs & child-resistant bottles
With growing consumer demands for health & wellness products, packaging aesthetics and barrier integrity are paramount. We offer pharmaceutical blister packs, HDPE bottles, stick packs, and eco-friendly recyclable cartons.
Core Capabilities & Deliverables:
How we take your product to commercial scale.
A disciplined, stage-gated manufacturing framework engineered to deliver pharmaceutical consistency with rapid time-to-market.
Discovery & Target Profiling
Active ingredient selection, standardisation assays, feasibility mapping, and raw material sourcing.
Bioavailability & Formulation
Organoleptic testing, pilot batches, pharmacokinetics optimization, and real-time dissolution assays.
Cleanroom Commercial Scaling
Automated Class 100,000 cleanroom production with zero cross-contamination and continuous QA batch records.
Packaging & Global Dispatch
High-barrier blister sealing, tamper-evident induction foil, certified CoAs, and expedited export dispatch.
Delivery Formats & Capabilities
Precision manufacturing delivery formats.
Equipped with pharmaceutical-grade automated production machinery operating inside certified ISO Class 8 cleanrooms.
Softgel Encapsulation
Automated nitrogen-blanketed rotary die encapsulation for fat-soluble vitamins, CoQ10, and algal oils.
DRCaps® Enteric Pellets
Delayed release acid-resistant capsules for targeted intestinal delivery of live probiotics and enzymes.
Effervescent & Soluble Powders
High-speed moisture-controlled cleanrooms for instant hydration and effervescent delivery formats.
Pectin & Vegan Gummies
Mogul-line starch-free depositing for sugar-free, gelatin-free nutraceutical gummy supplements.
Liquid Drops & Herbal Syrups
Ultrasonic extraction, amber glass packaging, and calibrated droppers for high-potency herbal actives.
Protein Blends & Micro-Milling
Instantized whey isolates, plant proteins, and micronized creatine with seamless powder dispersion.